Food Industry Automation
Food & Beverage
POA delivers food-safe automation, calibration, and compliance solutions that increase productivity and ensure purity across your operations.
Safety meets demand
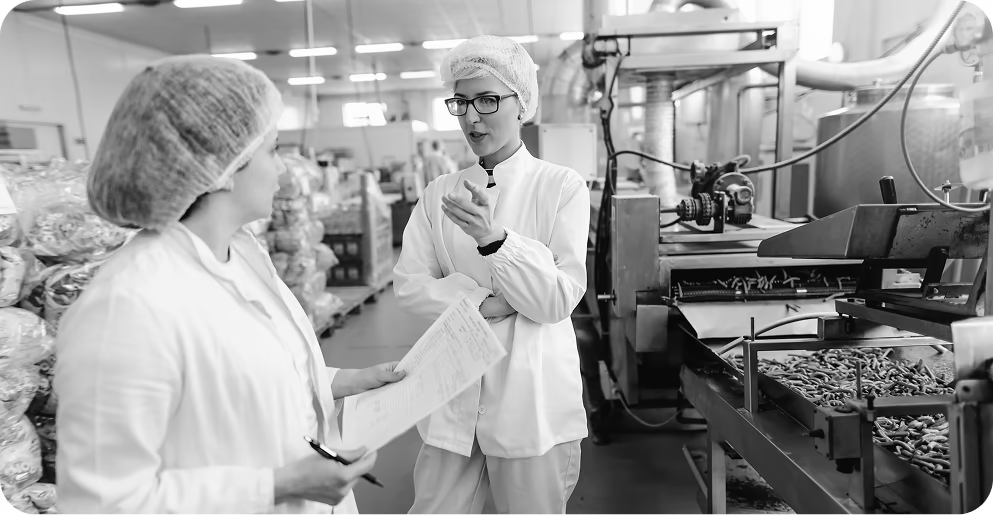
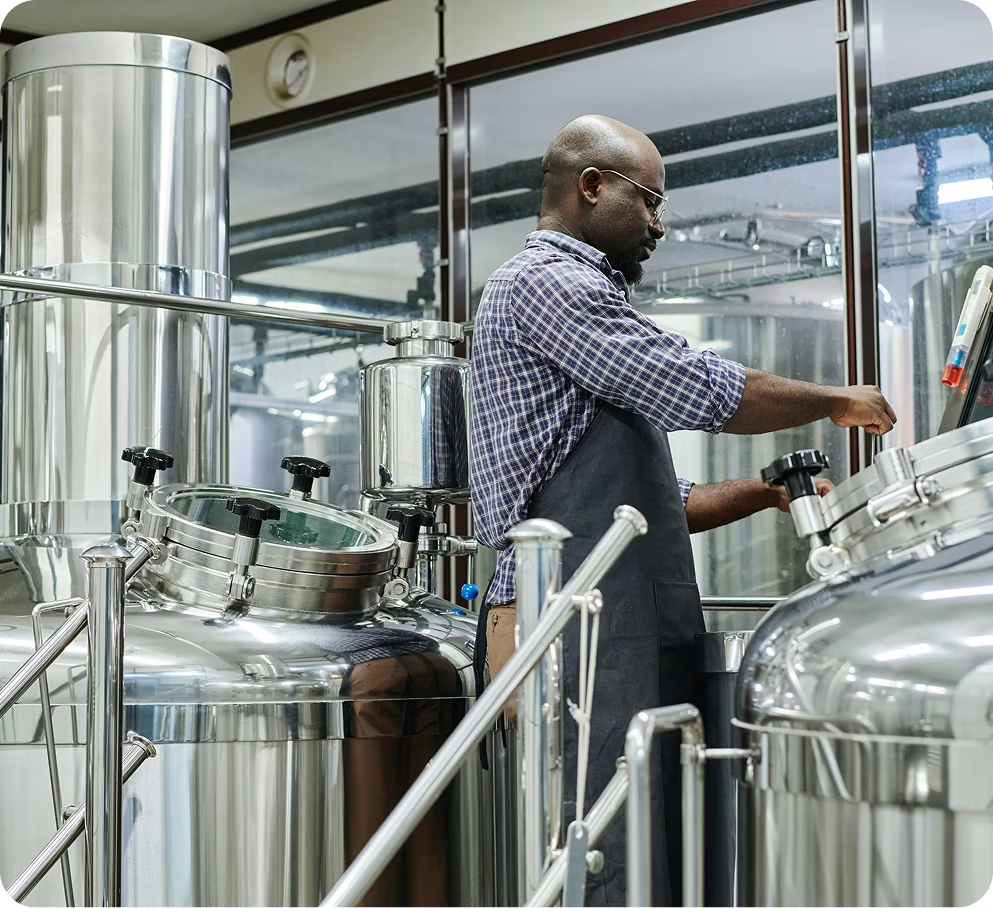
Your facility must meet strict FDA food safety regulations while maximizing throughput and minimizing labor costs. Every system needs precise temperature control, complete traceability, and documentation that satisfies auditors.
+ FDA regulations demand documented proof of safety
+ Manual processes slow production and increase costs
+ Temperature deviations risk product loss and recalls
+ Fragmented vendors create compliance gaps
One reliable partner
We design automation systems that protect product safety while increasing efficiency. Our team is trained in FDA Good Manufacturing Practices and understands food-grade requirements.
Food-Safe Automation Systems
+
We design and integrate conveyor controls, packaging automation, and robotic systems using food-grade components and sanitary-rated enclosures that meet FDA and USDA standards for direct food contact environments.
Temperature Monitoring & Control
+
From cold storage to pasteurization, we implement continuous temperature monitoring with automated alerts, data logging, and validation documentation proving your products stay within safe ranges throughout processing.
Traceability & Quality Systems
+
We integrate track-and-trace systems, batch recording, and automated quality checks that provide complete product traceability from raw materials through finished goods—critical for recall management and consumer safety.
Increase food safety & efficiency
Partner with one reliable company to deliver complete and compliant automation solutions.
Complete food safety solutions
From system design through ongoing monitoring, POA delivers integrated automation for food producers.

Integration
Design and build food-safe automated systems with sanitary-rated components and controls—ready for validation and production from day one.
Calibration
NIST-traceable calibration and asset management keeping your instrumentation accurate, compliant, and audit-ready throughout the year.
Validation
Comprehensive temperature mapping, equipment qualification, and testing documentation proving your systems meet food safety requirements.
"I have had the pleasure of working with Steve, [Lonnie, Edie] and the rest of the POA team for nearly 24 years now.
From filtration and calibration to validation and systems integration, POA has the staff, experience, and knowhow to deliver high quality results."
Ian Stout
Serán Bioscience
"POA is a critical partner in the continued success of our mobile gas generation project. Their team has consistently demonstrated exceptional technical leadership while providing deep industrial automation expertise that has directly influenced the quality, reliability, and performance of our system."
Tim Kemper
Director of Engineering, CV International
"Working with POA has felt less like engaging a vendor and more like adding trusted teammates to our project. Their professionalism, organization, and commitment to doing things right have made a lasting impact on our success."
Tim Kemper
Director of Engineering, CV International
"In February 2015, the McKesson drug distribution facility in Memphis, Tennessee experienced a roof collapse due to an ice storm. The damage...(threatened) the CDC's entire US supply of vaccines for children. With Steve and Lonnie leading, the entire POA team provided 24/7 support to McKesson. With POA's collaboration, McKesson was able to stabilize the situation, install a new controller, and get it operational. In this situation, partnering with the right company saved McKesson from a potential $876,000,000 loss."
Timothy Phelps, McKesson
Former Manager of Facilities & Engineering